Plant Shutdown Checklist: 40 Steps for a Safe, On-Time
Turnaround
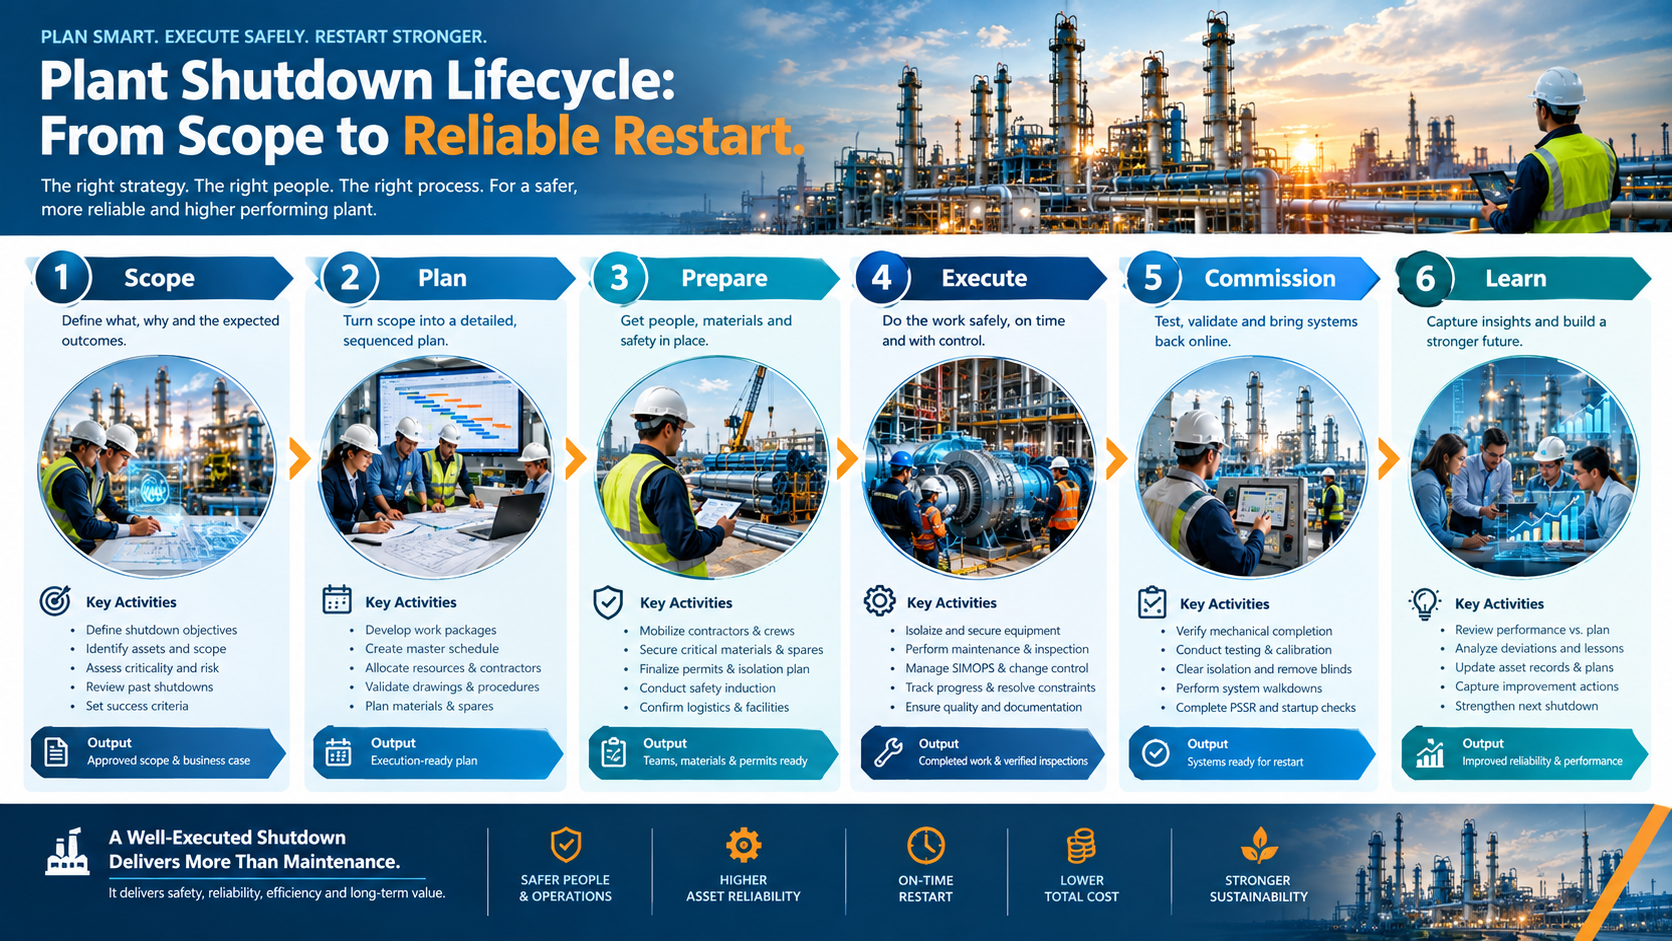
A shutdown maintenance checklist is more than a list of maintenance tasks. In a high-stakes industrial shutdown, it is the control framework that connects scope, safety, engineering, materials, contractors, inspections, execution, commissioning, and restart into one coordinated operating system.
A plant shutdown compresses weeks or months of maintenance work into a fixed production window. The objective is therefore not simply to complete more work. It is to complete the right work, in the right sequence, with the right resources, under controlled risk, and without extending the outage unnecessarily.
A disciplined shutdown maintenance checklist helps maintenance and operations leaders answer five questions before the first work permit is issued:
- What must be done?
- Why must it be done?
- Who owns it?
- What could prevent completion?
- What evidence proves the equipment is safe and ready to restart?
Why a Shutdown Maintenance Checklist Is a Strategic Reliability Tool
A plant shutdown is one of the few maintenance events where the organization has a scheduled opportunity to access equipment that normally cannot be isolated without affecting production.
That creates enormous value—but also enormous pressure.
Inspection teams may need access to vessels and piping. Mechanical teams may overhaul rotating equipment. Electrical teams may work on motors and switchgear. Instrumentation teams may calibrate critical loops. Contractors may perform specialist work. Operations must control isolation and de-isolation. EHS must manage permits and simultaneous operations. Procurement must ensure materials arrive before the workfront opens.
All of these activities compete for the same limited shutdown window.
The result is a system of dependencies.
A delayed valve overhaul can delay pressure testing. A failed inspection can create additional scope. A missing gasket can hold an entire work package. A contractor arriving late can disrupt the critical path. An incomplete punch list can delay startup authorization.
That is why effective shutdown planning begins well before the plant stops.
For major turnarounds, planning horizons can extend many months or even years depending on industry, regulatory requirements, asset criticality, and scope. MaintWiz’s strategic shutdown framework recommends progressively moving from strategic alignment to detailed planning, supply-chain lock-in, execution control, and post-shutdown learning.
The checklist below is designed as a practical control framework for manufacturing plants, process industries, utilities, power generation, chemicals, food and beverage, cement, oil and gas, and other asset-intensive environments.
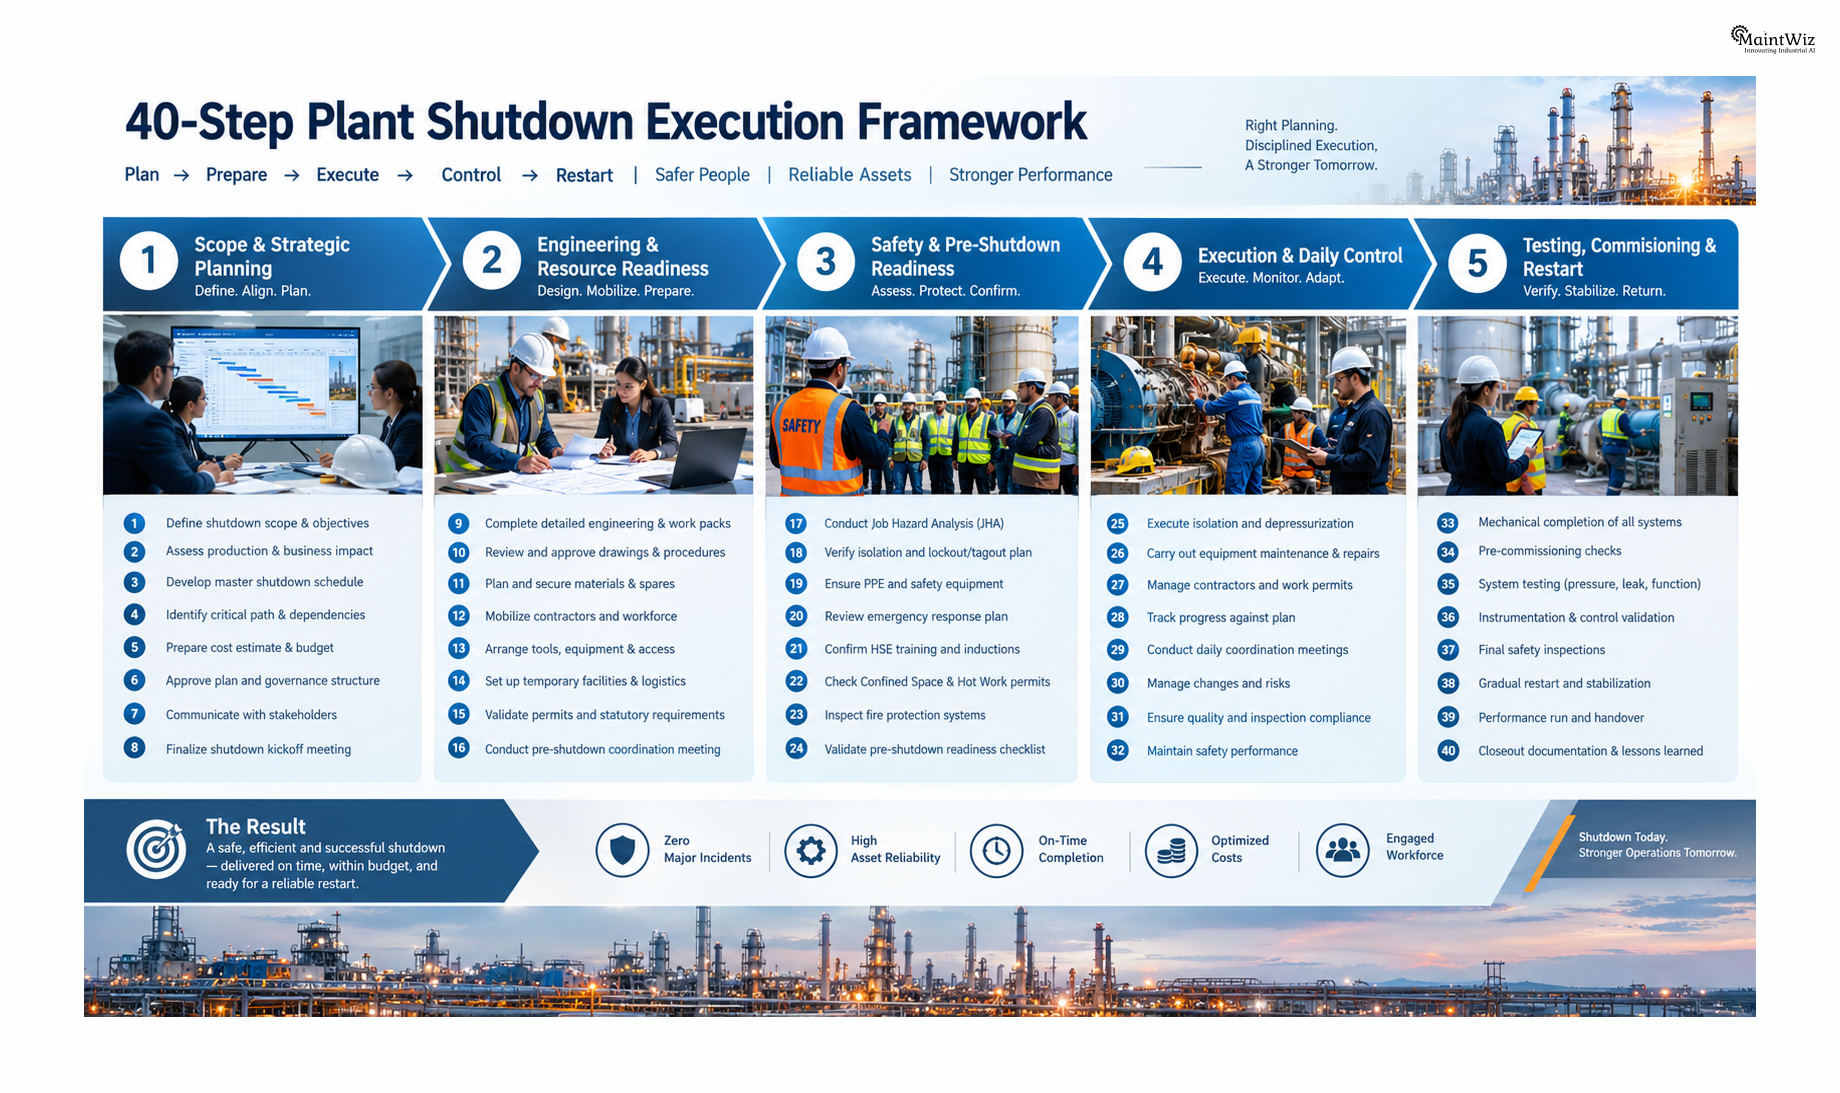
The 40-Step Shutdown Maintenance Checklist
Phase 1: Shutdown Scope and Strategic Planning
The first principle is simple: a shutdown is won before the shutdown begins.
Scope that is discovered during execution is expensive. Scope that is properly identified, risk-ranked, engineered, resourced, and prepared before execution is controllable.
1. Define the shutdown objective
Establish why the shutdown is being performed.
The objective may include statutory inspection, equipment overhaul, reliability improvement, preventive maintenance, debottlenecking, asset integrity work, cleaning, modification, or a combination of these.
Do not define the objective simply as “complete maintenance.” Establish measurable outcomes such as safe restart, targeted reliability improvement, compliance completion, zero critical punch items, or completion within a defined outage window.
2. Establish the shutdown window
Define the exact start and finish dates, operating constraints, production requirements, and restart deadline.
The shutdown window becomes the fundamental constraint for every subsequent planning decision.
3. Build the master shutdown scope
Create one controlled scope register containing all approved work.
Include:
- Maintenance work orders
- Inspection requirements
- Statutory work
- Reliability improvements
- Cleaning activities
- Engineering modifications
- Safety-critical work
- Deferred work
- Opportunity work
Avoid maintaining separate uncontrolled lists across spreadsheets, emails, engineering files, and contractor documents.
4. Review previous shutdown findings
Before creating new work, examine the previous shutdown report.
Look for:
- Deferred jobs
- Recurring failures
- Inspection findings
- Schedule overruns
- Contractor issues
- Material shortages
- Safety observations
- Quality problems
- Startup problems
- Lessons learned
A shutdown should be a learning cycle, not a recurring event with the organizational memory reset every time.
5. Perform asset criticality assessment
Rank equipment according to consequence of failure, safety exposure, production impact, environmental risk, redundancy, repair complexity, and regulatory significance.
Criticality should influence inspection depth, spare strategy, resource allocation, contingency planning, and execution priority.
6. Validate work orders
Every shutdown task should have a clear description, asset reference, scope, estimated duration, craft requirement, safety requirements, material requirements, and completion criteria.
Incomplete work orders create execution ambiguity.
7. Freeze the baseline scope
Establish a formal scope-freeze milestone.
After the freeze, additions should require documented approval with an explanation of safety, compliance, reliability, or production justification.
Scope control is one of the strongest defenses against uncontrolled turnaround growth.
8. Identify the critical path
Map task dependencies and determine which activities directly influence the restart date.
The critical path should receive disproportionate management attention because not every delayed activity has the same consequence.
Phase 2: Engineering, Work Packaging and Resource Readiness
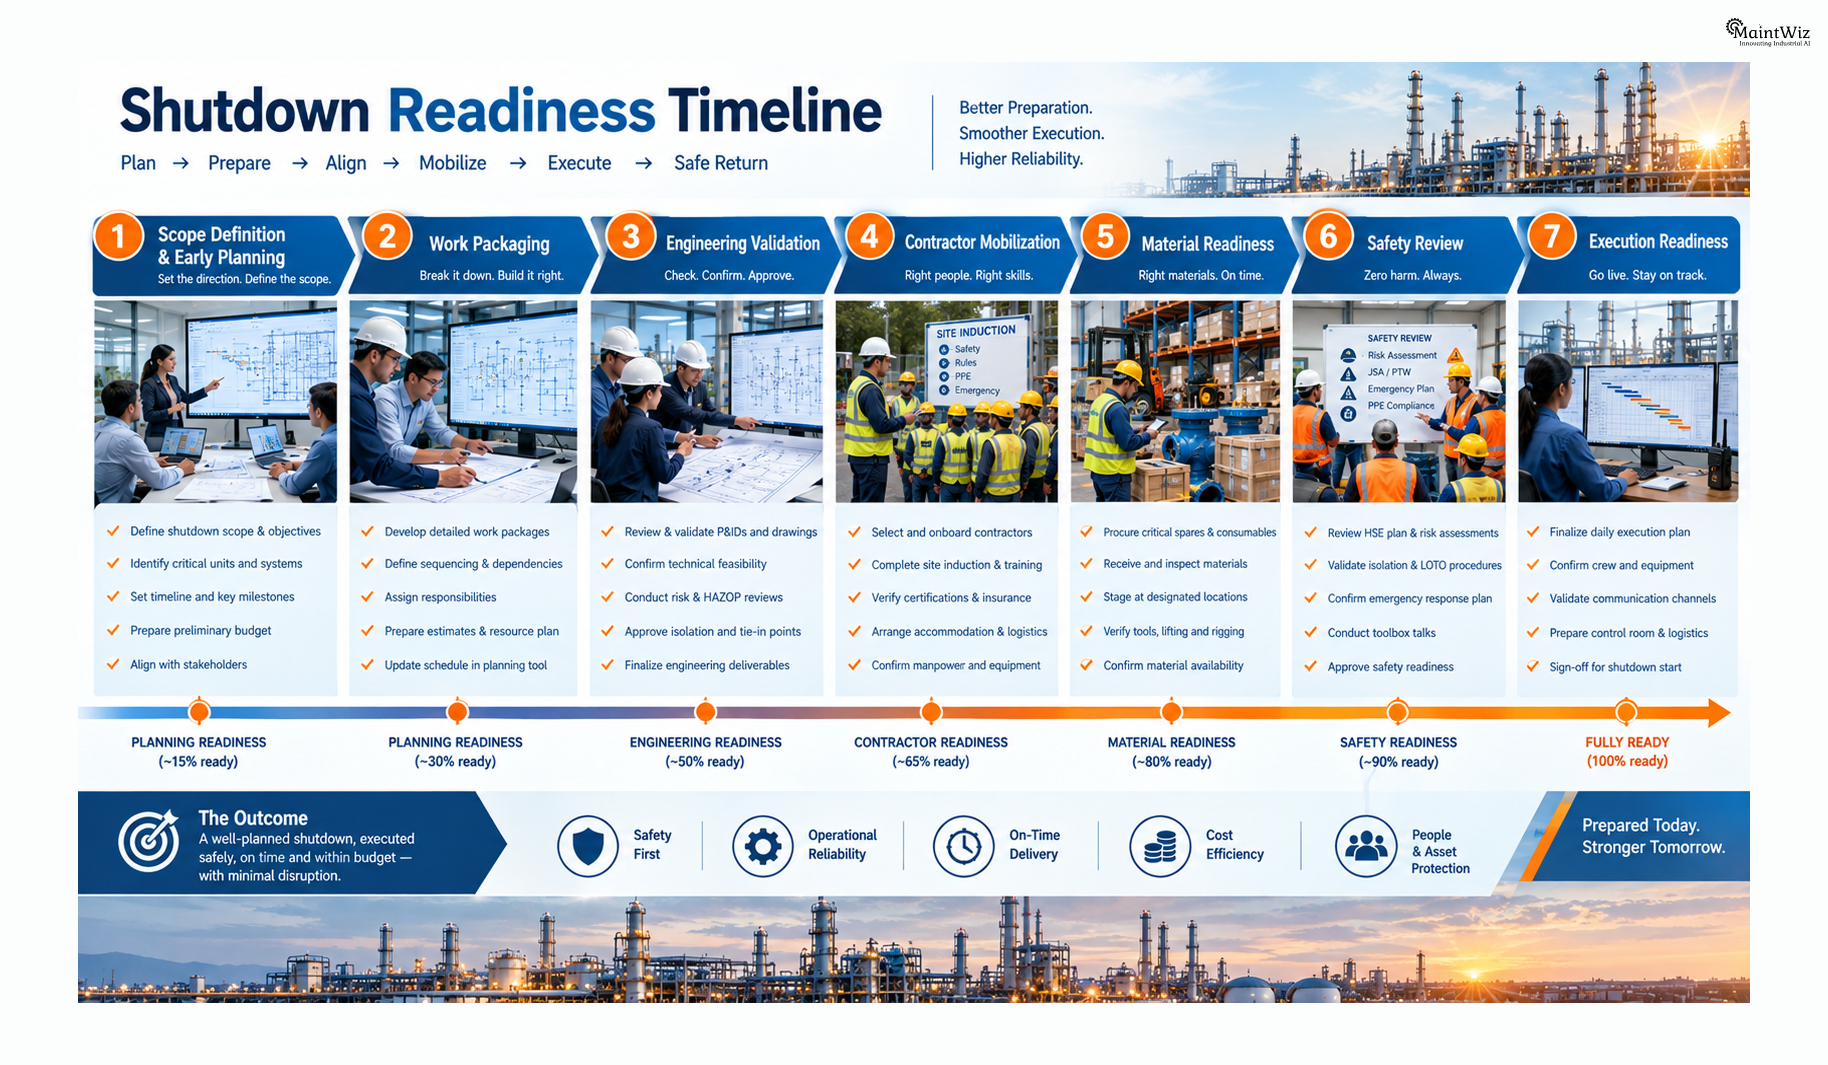
A good shutdown plan does not simply contain thousands of tasks. It converts them into executable work packages.
9. Develop detailed work packages
Break major work into field-ready packages.
Each package should define:
- Job steps
- Required tools
- Materials
- Drawings
- Procedures
- Permits
- Manpower
- Estimated duration
- Inspection requirements
- Quality acceptance criteria
10. Validate job estimates
Review planned labor hours and durations with experienced planners, supervisors, engineers, and technicians.
Historical actuals should be used wherever possible.
A shutdown schedule based entirely on optimistic estimates is not a schedule; it is a target.
11. Sequence interdependent work
Determine the correct order of isolation, cleaning, inspection, dismantling, repair, testing, reassembly, and commissioning.
Sequence matters because multiple trades may depend on the same equipment becoming available.
12. Confirm engineering drawings and procedures
Ensure current P&IDs, equipment drawings, electrical drawings, inspection procedures, torque specifications, maintenance instructions, and vendor documentation are available.
Outdated documentation can create both safety and quality risks.
13. Identify Management of Change requirements
Any modification that changes equipment design, process conditions, controls, materials, or operating procedures should be screened through the appropriate Management of Change process.
14. Confirm workforce requirements
Determine the required number of:
- Mechanical technicians
- Electrical technicians
- Instrumentation specialists
- Welders
- Inspectors
- Scaffolding crews
- Riggers
- Engineers
- Planners
- Supervisors
- Safety personnel
- Specialist contractors
Labor planning should consider day/night shifts, weekends, fatigue management, competency, and contingency coverage.
15. Mobilize contractors early
Contractors should be selected and mobilized according to technical capability, safety performance, workforce availability, certifications, and previous shutdown experience.
Contractor capacity should be confirmed before the shutdown window—not during it.
16. Confirm long-lead materials
Identify components whose absence could stop the critical path.
Typical examples include:
- Large valves
- Bearings
- Mechanical seals
- Heat-exchanger components
- Motors
- Specialty gaskets
- Instrumentation
- Electrical components
Material readiness should be verified physically, not merely assumed from a purchase order.
Phase 3: Safety, Isolation and Pre-Shutdown Readiness
Shutdowns create concentrated risk because normal operating barriers are changed while large numbers of people perform non-routine work.
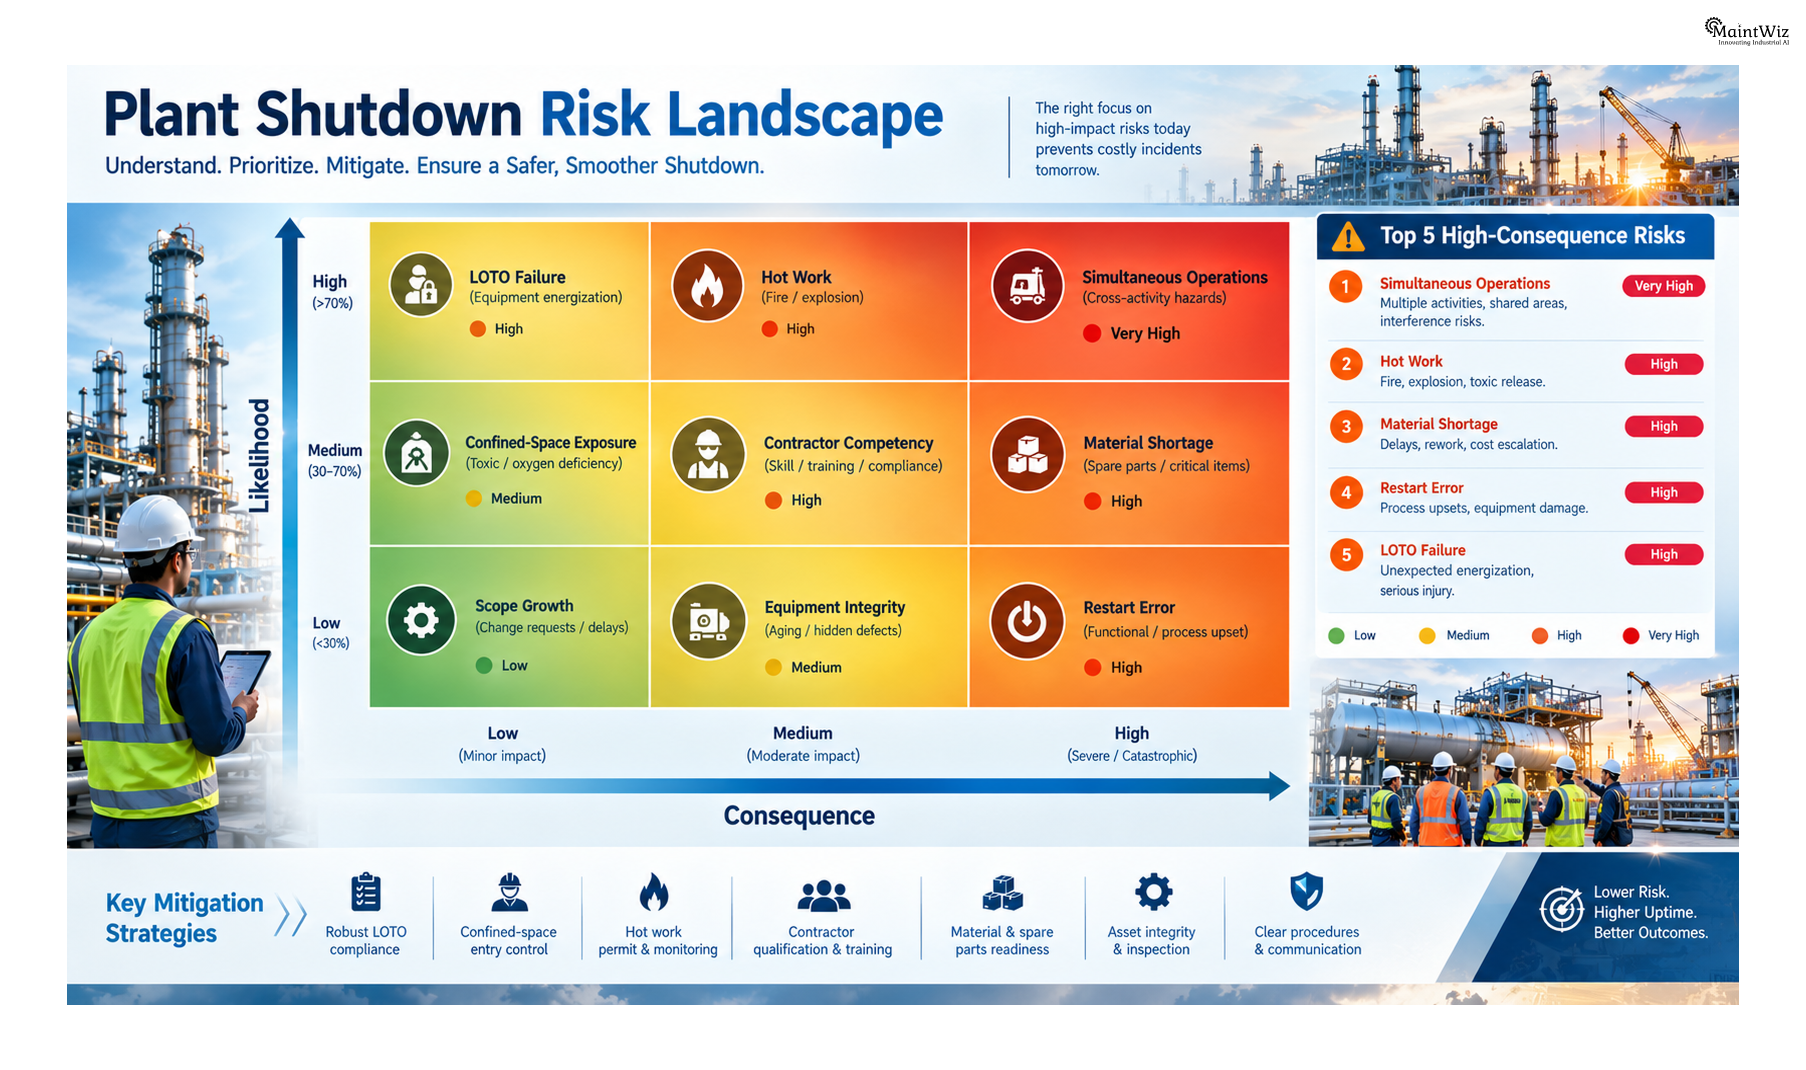
MaintWiz’s shutdown safety guidance highlights non-routine work, simultaneous operations, changing operating conditions, and increased contractor presence as important shutdown risk factors.
17. Build the shutdown risk register
Identify technical, safety, environmental, schedule, material, contractor, quality, and restart risks.
For every major risk, define:
Risk → Trigger → Preventive control → Owner → Contingency
18. Confirm isolation philosophy
Identify all energy sources that must be isolated before work begins.
This includes electrical, mechanical, hydraulic, pneumatic, thermal, chemical, pressure, gravity, stored energy, and process energy.
19. Verify LOTO requirements
Lockout/tagout or the site’s equivalent energy-isolation process must be defined for applicable equipment.
Isolation status must be controlled and independently verified according to site procedures.
20. Prepare permit requirements
Identify required permits before execution.
Depending on the facility, this may include:
- Hot work
- Confined space
- Line breaking
- Electrical work
- Work at height
- Excavation
- Lifting
- Radiation
- Chemical handling
21. Conduct contractor safety induction
Every contractor must understand site rules, emergency arrangements, restricted areas, PPE requirements, permit processes, reporting requirements, and stop-work authority.
22. Plan simultaneous operations
Map activities that could interact with each other.
Examples include:
- Hot work near chemical cleaning
- Lifting near energized work
- Scaffolding near operating equipment
- Confined-space entry near adjacent work
- Multiple contractors working in one process area
SIMOPS control is particularly important during peak shutdown activity.
23. Conduct pre-shutdown readiness review
Before the plant enters the shutdown window, verify that scope, people, materials, permits, equipment, procedures, logistics, safety controls, and communication channels are ready.
A readiness review should result in explicit Go / No-Go decisions for major work fronts.
Phase 4: Shutdown Execution and Daily Control
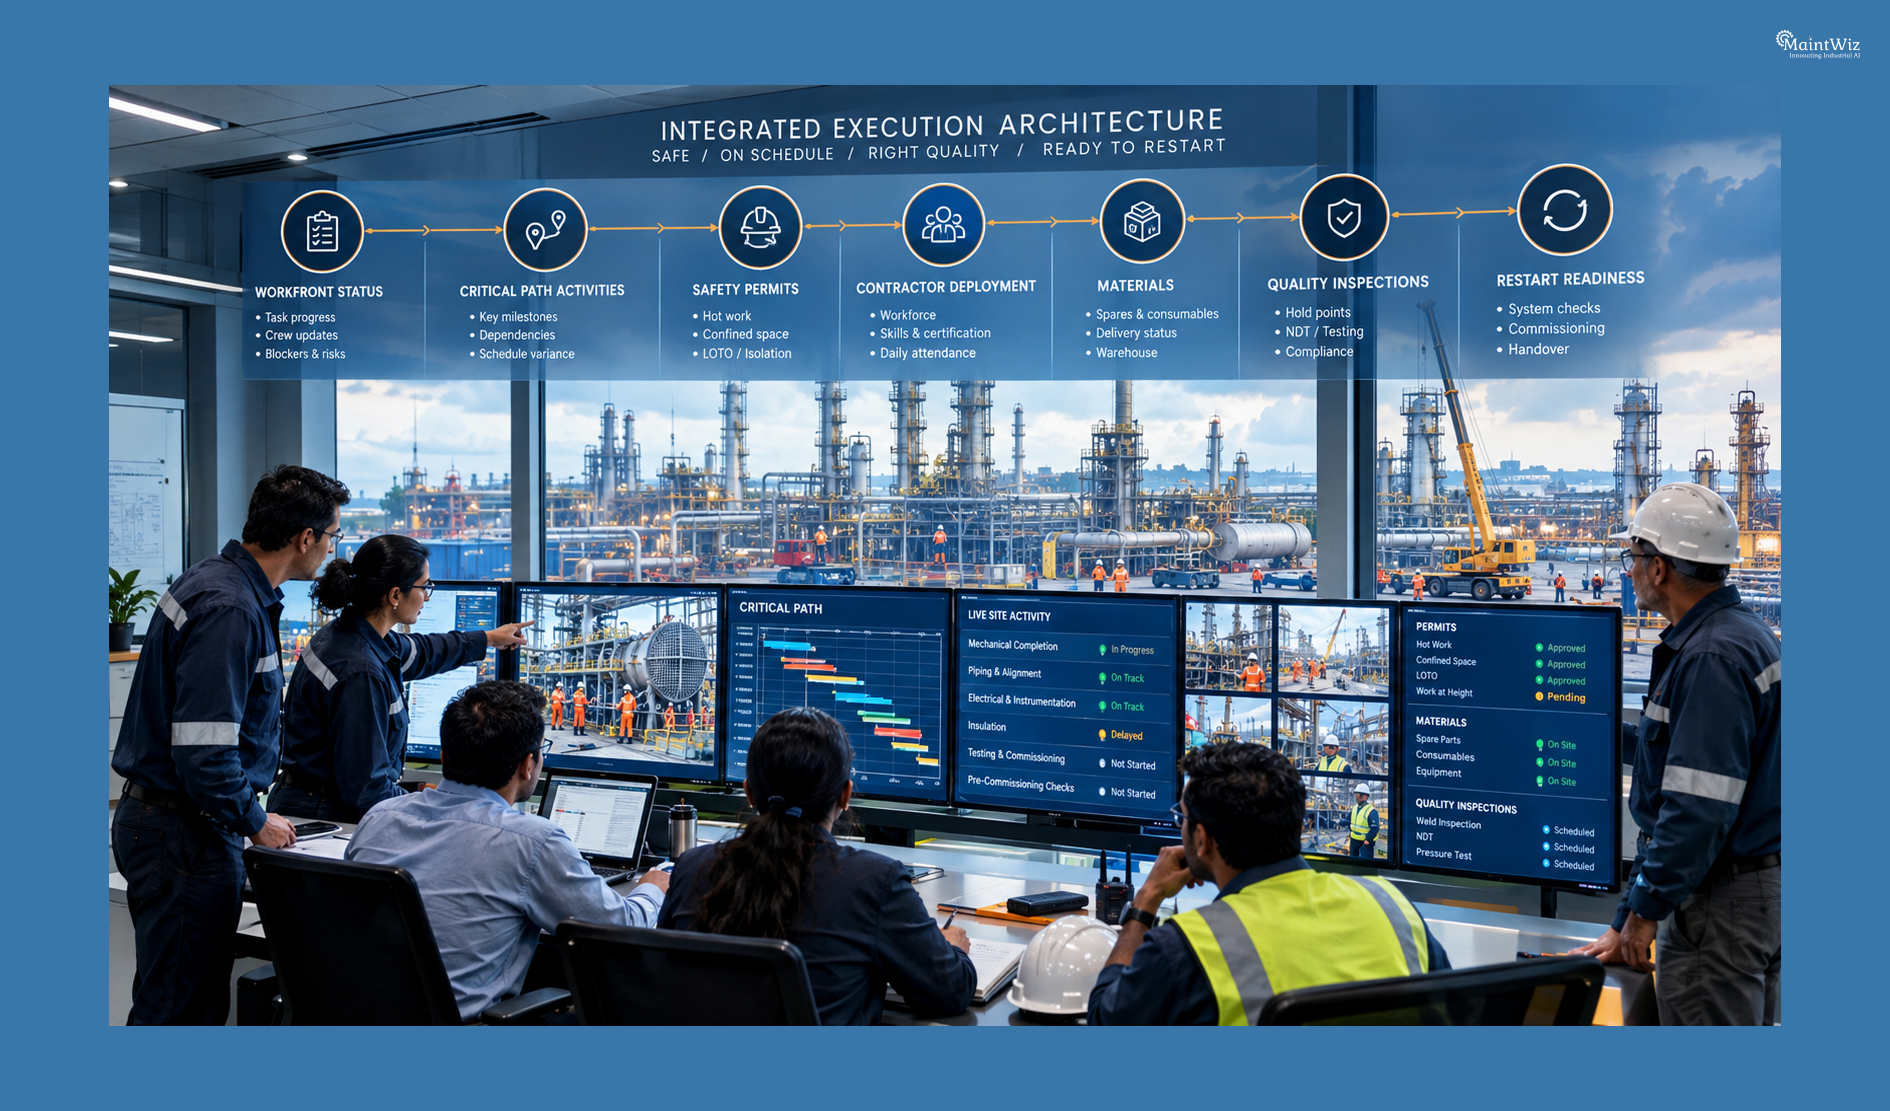
Once the plant stops, the nature of management changes.
The question is no longer “Are we prepared?”
It becomes:
“Are we still on the path to safe, on-time restart?”
24. Execute controlled plant shutdown
Operations should follow the approved shutdown sequence.
Equipment should not be handed to maintenance until the required isolation, depressurization, draining, cleaning, purging, and verification activities are complete.
25. Establish the shutdown control room
Create a central control point for:
- Schedule
- Work-front status
- Safety
- Critical path
- Resource conflicts
- Material shortages
- Scope changes
- Quality issues
- Restart readiness
26. Conduct daily shutdown meetings
Daily meetings should be short, decision-oriented, and data-driven.
Review:
- Planned versus actual work
- Critical-path status
- Safety events
- Permit constraints
- Material shortages
- Contractor performance
- Quality holds
- New scope
- Recovery actions
MaintWiz’s daily shutdown management framework emphasizes clear daily objectives, dynamic change control, and unified situational awareness across maintenance, operations, engineering, and contractors.
27. Track progress against the baseline
Measure actual progress against the approved shutdown schedule.
Do not rely solely on percentage-complete estimates. Validate progress through completed work, inspection sign-offs, test records, and quality documentation.
28. Control emergent work
Shutdown inspections frequently reveal additional defects.
Not every defect should automatically become shutdown scope.
Evaluate emergent work against:
- Safety consequence
- Regulatory requirement
- Production risk
- Reliability impact
- Restart risk
- Available time
- Required resources
Then formally approve, defer, or reject it.
29. Protect the critical path
When a critical-path task slips, initiate recovery immediately.
Possible responses include:
- Additional shifts
- Resource reallocation
- Alternative work sequencing
- Specialist mobilization
- Parallel execution
- Material escalation
- Engineering decision support
The goal is not to hide schedule variance. It is to act before variance becomes an irreversible restart delay.
30. Perform quality hold-point inspections
Critical work should have predefined inspection and acceptance points.
For example:
Repair → Inspection → Testing → Acceptance → Reassembly
Equipment should not move to the next stage without required quality evidence.
31. Maintain a live punch list
Record incomplete or defective work continuously.
Classify punch items according to their impact on safe startup and reliable operation.
A punch list that is created only at the end of the shutdown is usually a symptom of weak completion control.
Phase 5: Testing, Commissioning and Safe Restart
Restart is not simply the reverse of shutdown.
It is a new risk phase because equipment, piping, instrumentation, electrical systems, controls, and process conditions are being returned to service.
32. Verify mechanical completion
Confirm that equipment has been correctly reassembled and that required inspections, torque checks, lubrication, guards, supports, alignment, and documentation are complete.
33. Complete pressure and functional testing
Perform applicable pressure, leak, electrical, instrumentation, control-loop, functional, and system tests.
Results should be recorded and traceable.
34. Verify blind and isolation status
Maintain a controlled record of blinds, blanks, isolations, temporary connections, and removed protections.
Before re-energization or pressurization, verify the approved configuration.
35. Conduct system walkdowns
Operations, maintenance, engineering, and safety representatives should inspect systems before startup.
Check for:
- Loose tools
- Foreign objects
- Open drains
- Incorrect valve positions
- Missing guards
- Temporary hoses
- Unconnected instruments
- Unfinished insulation
- Incorrect electrical connections
36. Close critical punch items
Critical startup-related punch items should be formally verified before startup authorization.
Non-critical items should have an accountable owner and approved post-startup completion plan.
37. Conduct Pre-Startup Safety Review
A formal PSSR or equivalent review should confirm that modified or maintained systems are ready for operation.
The review should consider technical completion, safety controls, procedures, training, documentation, alarms, interlocks, emergency systems, and operating readiness.
38. Execute controlled restart
Restart systems in the approved sequence rather than attempting to bring the entire plant back online simultaneously.
Monitor equipment behavior closely during the first operating period.
39. Monitor post-startup performance
The shutdown is not complete when production resumes.
Track:
- Equipment temperature
- Vibration
- Pressure
- Flow
- Energy performance
- Quality
- Alarms
- Repeated failures
- Production stability
- Abnormal operating conditions
Post-startup monitoring can identify defects that were not visible during static inspection.
40. Capture lessons learned and update the reliability system
The final step is organizational learning.
Review:
- Schedule performance
- Cost variance
- Safety performance
- Scope growth
- Contractor performance
- Material availability
- Inspection findings
- Repeat failures
- Startup problems
- Quality issues
- Planning accuracy
Then update the CMMS, asset history, maintenance plans, job plans, checklists, risk registers, spare strategies, and future shutdown scope.
A shutdown should leave the organization with better knowledge than it had before the shutdown. MaintWiz’s shutdown continuous-improvement guidance similarly emphasizes converting shutdown findings into structured knowledge, future checklists, maintenance planning, and repeatable improvement.
The Shutdown Checklist Is Only as Strong as Its Critical-Path Logic
A common mistake is treating all 40 steps as equally important.
They are not.
The most important shutdown activities are those that influence one or more of these four outcomes:
Safety → Scope → Schedule → Restart Reliability
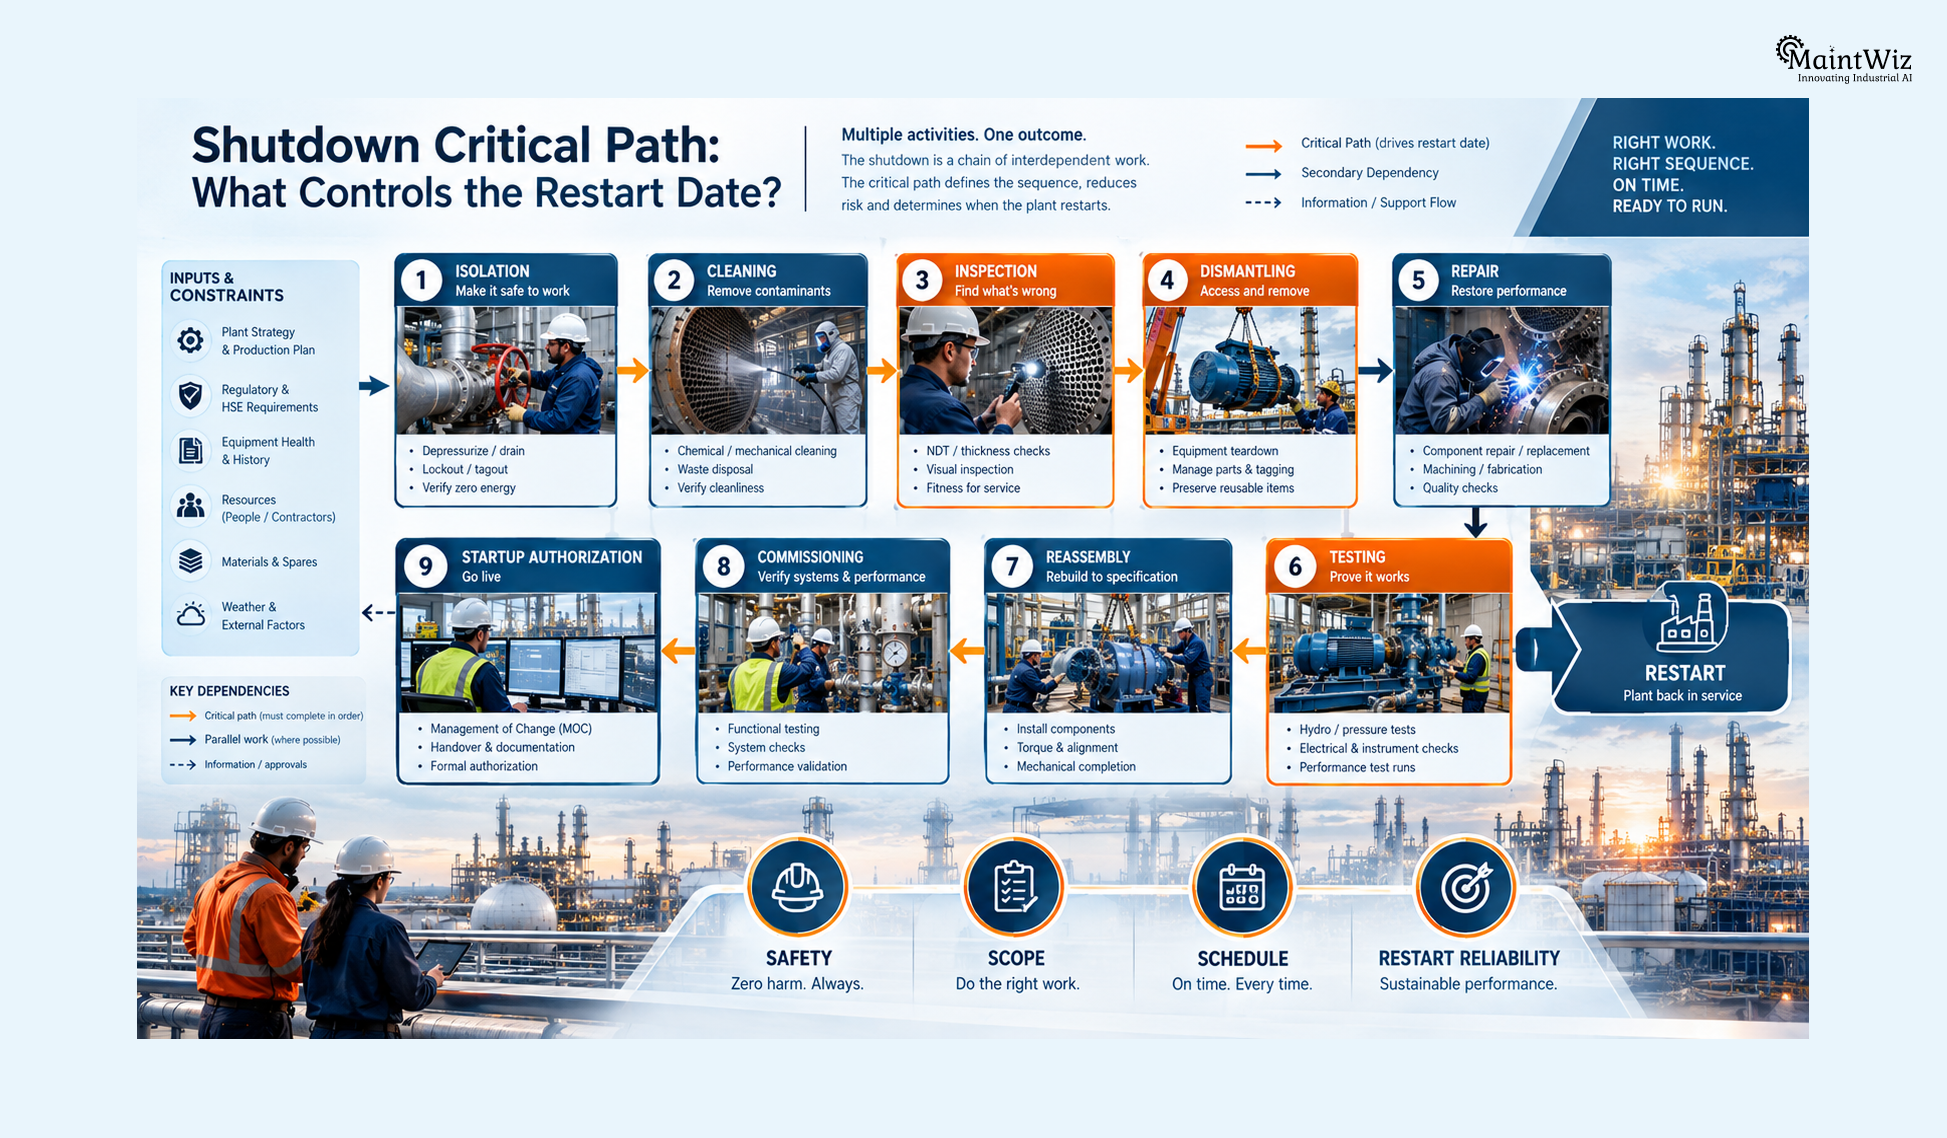
A practical prioritization model is:
Risk × Criticality × Dependency × Consequence
A high-criticality pump overhaul that sits directly on the restart path deserves far more management attention than a low-risk housekeeping activity that can be completed independently.
This is why shutdown management should move beyond task completion toward constraint management.
The question should not be:
“How many work orders are complete?”
The stronger question is:
“Which unresolved constraint can prevent the plant from restarting safely and on time?”
Shutdown KPIs That Actually Matter
A shutdown can finish on the scheduled date and still be unsuccessful if the organization achieved the date through excessive overtime, uncontrolled scope reduction, poor quality, or unresolved reliability problems.
Use a balanced KPI framework.
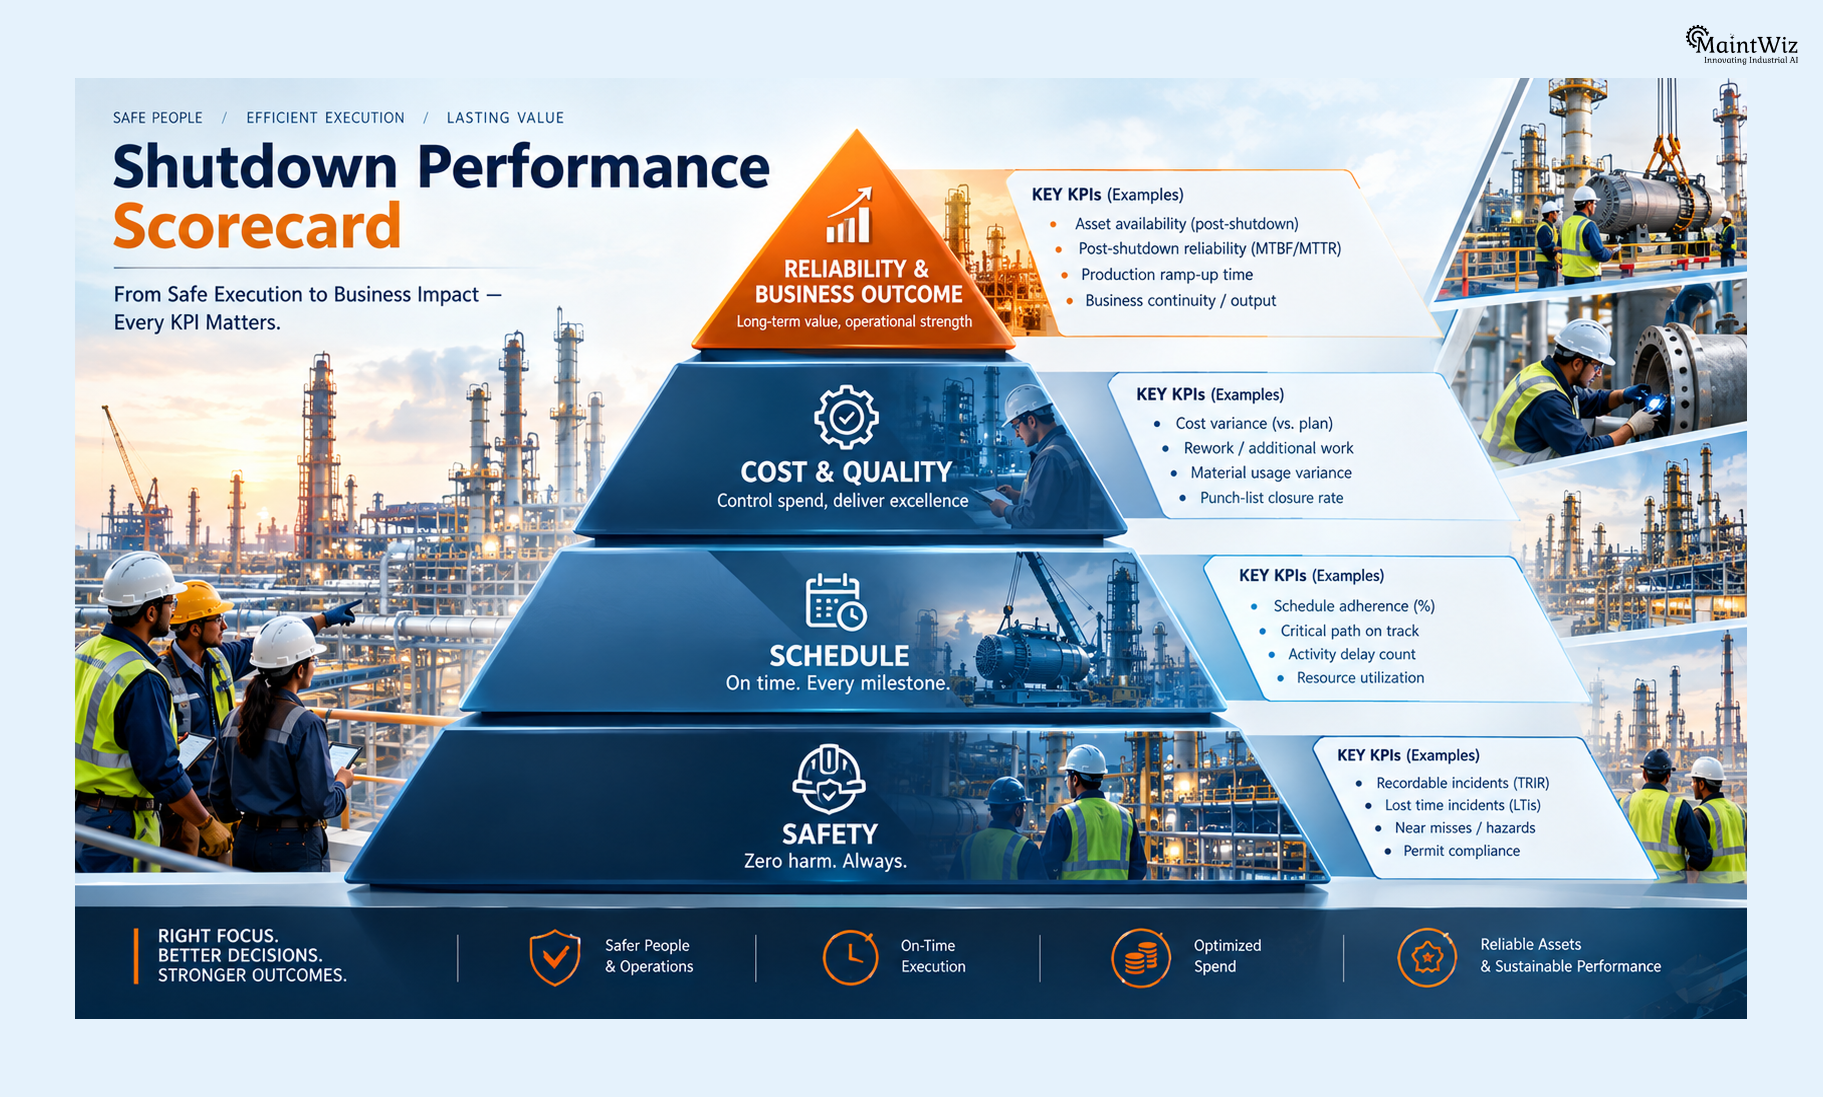
Safety
- Recordable incidents
- Permit deviations
- LOTO compliance
- Safety observations
- High-potential near misses
Schedule
- Schedule adherence
- Critical-path variance
- Planned versus actual duration
- Work-order completion
- Daily productivity
- Restart readiness
Cost
- Shutdown budget versus actual
- Contractor cost
- Overtime
- Material cost
- Emergent-scope cost
- Cost of schedule extension
Quality
- First-time acceptance
- Rework
- Inspection failures
- Punch-list volume
- Repeat failures after startup
Reliability
- Post-shutdown MTBF
- Asset availability
- Failure recurrence
- Equipment health
- OEE impact
- Maintenance backlog
The KPI principle is simple: measure the shutdown as a business event, not merely as a maintenance project. MaintWiz’s maintenance KPI framework similarly connects reliability, maintenance execution, financial efficiency, and predictive-maintenance indicators rather than relying on work-order counts alone.
How CMMS Technology Strengthens Shutdown Execution
A spreadsheet can contain a shutdown checklist.
The problem is not storing the checklist.
The problem is controlling thousands of relationships between assets, tasks, people, permits, materials, dependencies, inspections, costs, and completion evidence.
A CMMS provides the operational structure for that control.
A shutdown-enabled CMMS should help teams maintain a single source of truth for:
- Asset hierarchy
- Shutdown work orders
- Job plans
- Maintenance history
- Work packages
- Labor
- Contractors
- Materials
- Spare parts
- Safety checklists
- Inspections
- Schedules
- Progress
- Costs
- Punch lists
- Completion records
This is especially important because shutdown execution generates information that must remain useful after the plant restarts.
How MaintWiz CMMS Supports Shutdown Maintenance
MaintWiz CMMS is relevant to shutdown execution because it connects planning, work management, safety, inventory, progress monitoring, and post-shutdown asset information within a digital maintenance environment.
Its shutdown capabilities include structured shutdown procedures and checklists, real-time progress monitoring, performance analytics, equipment-integrity verification, testing protocols, and controlled production restart support.
Shutdown planning and work management
MaintWiz can help organize shutdown activities around work orders, schedules, assets, resources, and execution priorities. Its maintenance-planning capabilities provide equipment calendars and scheduling visibility that can help maintenance teams coordinate work around operational constraints.
Safety and compliance
Shutdown work requires more than technical task completion. MaintWiz’s shutdown capabilities include safety checklists, compliance tracking, contractor coordination, and field access to work orders and checklists.
Materials and spare parts
Shutdown delays frequently originate outside the maintenance workshop. A missing bearing, gasket, seal, valve, instrument, or specialist tool can hold an otherwise ready workfront.
Digital inventory visibility helps connect shutdown work orders to required materials and availability.
Execution visibility
During a shutdown, management needs to know which workfronts are progressing, which are blocked, and which threaten the critical path.
Real-time progress monitoring provides a stronger management model than waiting for end-of-shift spreadsheets.
The 90-day shutdown readiness sprint
MaintWiz can also support a focused 90-day readiness approach:
Days 1–30: Build the asset and work-order baseline, validate scope, identify critical assets and establish shutdown KPIs.
Days 31–60: Build work packages, schedule resources, confirm materials, establish checklists, and close planning gaps.
Days 61–90: Conduct readiness reviews, monitor outstanding constraints, confirm contractor and material readiness, and prepare execution dashboards.
The value of the CMMS is therefore not simply digitization. Its strategic value is creating a traceable chain from shutdown scope to field execution to verified asset condition and future maintenance decisions.
A Better Way to Think About Shutdown Readiness
The traditional question is:
“Are we ready for the shutdown?”
A more rigorous question is:
“Can every critical workfront demonstrate readiness?”
For each critical work package, verify six dimensions:
| Readiness Dimension | Key Question |
|---|---|
| Scope | Is the work clearly defined and approved? |
| People | Are qualified resources available? |
| Materials | Are all critical parts physically available? |
| Safety | Are permits, isolation and risk controls ready? |
| Method | Are procedures, drawings and job plans complete? |
| Completion | Are inspection and acceptance criteria defined? |
A work package that fails one of these tests should not be considered execution-ready.
This approach moves shutdown planning from calendar readiness to workfront readiness.
From Shutdown Checklist to Shutdown Operating System
The best industrial organizations do not treat the checklist as a document that someone prints and ticks.
They treat it as an operating system for the event.
That means every checklist item has:
An owner → a deadline → a dependency → an acceptance criterion → evidence of completion
This creates accountability.
It also creates data.
Over multiple shutdown cycles, the organization can compare:
- Planned versus actual duration
- Planned versus actual labor
- Forecast versus actual materials
- Contractor productivity
- Repeat defects
- Scope growth
- Inspection findings
- Critical-path disruptions
- Startup performance
That information becomes increasingly valuable.
The first shutdown produces a checklist.
The second produces a better checklist.
The third produces a benchmark.
Eventually, the organization develops a shutdown knowledge system.
That is where shutdown management becomes a strategic reliability capability rather than a recurring emergency.
Conclusion: A Safe Shutdown Is Planned Long Before the Plant Stops
A plant shutdown should never be judged simply by whether the equipment was repaired.
The real measure is whether the organization achieved the intended reliability, safety, quality, schedule, and financial outcomes without compromising the integrity of the restart.
A robust shutdown maintenance checklist therefore has four jobs:
- Prepare the organization before the outage.
- Control risk and execution during the outage.
- Verify equipment before restart.
- Convert shutdown experience into future reliability improvement.
The 40 steps in this framework provide a practical backbone—from defining scope and criticality to controlling work packages, contractors, permits, materials, inspections, critical-path activities, commissioning, restart, and lessons learned.
But the deeper principle is more important than any individual checklist item:
Shutdown performance is determined by the quality of decisions made before the shutdown, the discipline applied during execution, and the learning captured after restart.
When those three elements are connected through disciplined planning and a digital maintenance system, a shutdown stops being a disruptive maintenance event and becomes a strategic opportunity to reset asset reliability, strengthen operational resilience, and improve long-term plant performance.
Frequently Asked Questions
What is a shutdown maintenance checklist?
A shutdown maintenance checklist is a structured set of planning, safety, maintenance, inspection, execution, commissioning, and restart activities used to control a planned industrial shutdown. It ensures that critical tasks, dependencies, resources, permits, materials, inspections, and completion requirements are systematically managed.
How far in advance should a plant shutdown be planned?
The appropriate planning horizon depends on shutdown complexity. Routine planned shutdowns may require weeks or months, while major turnarounds can require much longer strategic preparation. MaintWiz’s shutdown planning framework describes a 12-month strategic approach for complex industrial shutdowns, with progressively more detailed planning as execution approaches.
What should be included in a plant shutdown checklist?
A comprehensive checklist should cover scope definition, asset criticality, work orders, engineering, work packages, contractors, materials, permits, LOTO, risk management, SIMOPS, execution, progress tracking, quality inspections, punch lists, testing, commissioning, PSSR, restart and lessons learned.
What is the difference between shutdown, turnaround and outage?
A shutdown generally refers to a planned cessation of operations to perform maintenance or other work. A turnaround is typically a larger, more complex planned event involving extensive inspection, maintenance, repair, modification, and asset-integrity activities. An outage is a broader term for a period when equipment or production is unavailable. The exact terminology varies by industry. MaintWiz’s comparison distinguishes these events by planning horizon, scope, governance, trigger and risk profile.
How do you keep a plant shutdown on schedule?
Control the baseline scope, identify the critical path, prepare work packages early, verify materials and contractors, track progress daily, manage emergent work formally, escalate constraints quickly, and maintain a live recovery plan for critical-path delays.
What are the most important shutdown safety checks?
Critical safety controls include energy isolation, LOTO, confined-space controls, hot-work permits, line-breaking controls, lifting safety, work-at-height requirements, contractor competency, SIMOPS management, emergency preparedness, and pre-startup safety verification.
How do you control shutdown scope creep?
Freeze the baseline scope before execution and require formal approval for additions. Each emergent job should be evaluated against safety, compliance, reliability, production, restart, resource, and schedule consequences.
How can CMMS improve shutdown maintenance?
A CMMS can centralize assets, work orders, job plans, schedules, resources, spare parts, safety checklists, inspections, progress, costs, and completion history. This provides greater visibility and traceability throughout the shutdown lifecycle.
What shutdown KPIs should plant managers track?
Plant managers should track safety performance, schedule adherence, critical-path variance, cost variance, work completion, emergent scope, contractor productivity, quality and rework, punch-list status, restart readiness, asset availability, and post-shutdown reliability.
How can MaintWiz support plant shutdown execution?
MaintWiz provides shutdown-oriented capabilities for procedures and checklists, work management, progress monitoring, safety and compliance, inventory, equipment testing, analytics, and controlled restart.
Jai Balachandran is an industry expert with a proven track record in driving digital transformation and Industry 4.0 technologies. With a rich background in asset management, plant maintenance, connected systems, TPM and reliability initiatives, he brings unparalleled insight and delivery excellence to Plant Operations.
Company
Download App